

Latest Products



Contact Us
- The Fourth Floor, A-A3 Zone, Aviation Business Area, DongLi Distrct, Tianjin, China.
- >salesmanager@coilwinding machinechina.com
- +8613072088960


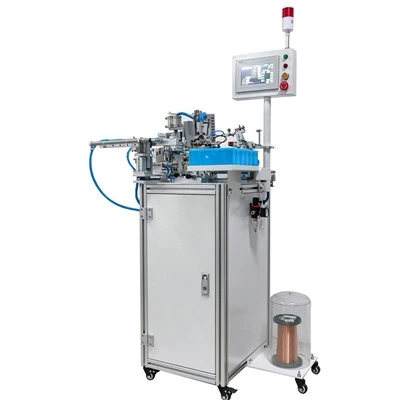

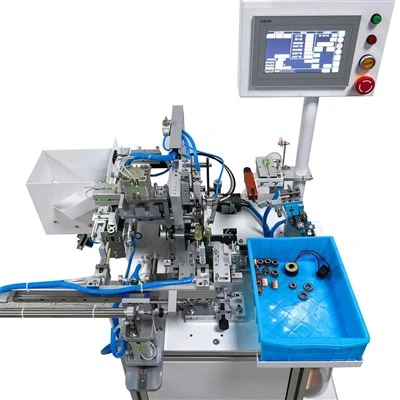


Toroidal Core Winding Machine For Current Transformer
Model:GW-7004
Max. wire diameter:0.2mm
Min. wire diameter:0.05mm
Max. finished O.D.:35mm
Min. finished O.D.:6mm
Max. finished product height:20mm
Description
GW‑7004 Fully‑Automatic Toroidal Coil Winding Machine
Product Overview
Grewin GW‑7004 and GW‑7005 are slider‑driven fully‑automatic toroidal coil winding machines, designed for mass‑volume production of small‑size toroidal transformers, common‑mode inductors, differential coils, and EMI filter cores.
Unlike semi‑automatic toroidal winders, this unit completes the full workflow: automatic core feeding, wire storage & winding, wire cutting, waste‑copper‑wire removal, and finished‑core unloading.
All maintenance guidance and fault‑handling content on this page is summarized from real‑life after‑sales cases collected from global customer production sites. We have documented dozens of recurring on‑site issues and practical fixes in our official operation manual, helping factory technicians reduce production downtime.
This winding equipment is widely deployed among electronics manufacturers producing power supplies, PCB‑mount inductors, miniature current transformers, and consumer‑electromagnetic components.
Main Technical Parameters
| Item | Specification |
|---|---|
| Model | GW‑7004 |
| Input Power | 110V‑220V, 50/60Hz |
| Working Air Pressure | 0.5‑0.7 MPa |
| Applicable Wire Gauge | 0.05 mm‑0.2 mm enameled copper wire |
| Magnetic Core Outer Diameter | 6 mm‑35 mm |
| Max Coil Height | 20 mm |
| Winding Speed | Stepless adjustable, max 1400 RPM |
| Control System | PLC + Touch‑screen HMI + Servo drive |
| Program Backup | USB flash‑disk program copy & duplication |
| Machine Dimension | 1100 × 900 × 1700 mm |
| Net Weight | 720 kg |


Core Machine Features
1. Full‑automatic production workflow
Auto-feed, wind, cut wire, clean scrap copper, and unload finished cores. Greatly reduces manual labor for high‑volume toroidal coil manufacturing.
2. USB program copy function
You can copy complete winding parameters via a USB stick. Fast program duplication across multiple production machines when you run identical products.
Operation tip: Please switch the HMI interface to the Chinese version first before performing USB program copy, following our tutorial video.
3. Rich real‑time alarm & practical troubleshooting database
The HMI outputs clear alarm prompts when failures happen. Our manual records real‑world faults reported by overseas customers: shuttle yellow marker fading, magazine stopping mid‑cycle, slider unexpected closing, wire‑cut failure, scrap‑copper triggering false differential‑coil alarms, unloading malfunctions, and sensor breakdowns. Technicians can follow step‑by‑step illustrated solutions.
4. Modular replaceable wearing parts
Slider, shuttle (wire‑storage ring), wool felt, guide pins, fixtures and sensors can be swapped for different core sizes. Spare‑part supply is available long‑term.
5. Stable pneumatic‑electrical integration
Cylinders, magnetic sensors and through‑beam sensors form the core detection system; all key components are selected for continuous 24‑hour factory‑shop operation.
6. Customization support
Custom tooling and winding logic modification for non‑standard toroidal magnetic‑core requirements.

Typical Application
- Small toroidal transformer mass‑production
- Common‑mode inductor & differential coil winding
- EMI filter coil for switching power supply
- Miniature current‑transformer core winding
- Electromagnetic component OEM & contract‑manufacturing workshops
Real‑World Troubleshooting From Customer Production Sites
The problems below are actual issues submitted by end‑users during daily mass‑production, extracted from our GW‑7004 / GW‑7005 service manual. Operators can perform basic inspection before calling for technical support.
1. Shuttle yellow sensing mark wears away
Symptom:
Machine pops up errors: "Opening not found", "The retraction cylinder of the wire is not fully retracted". The yellow positioning paint mark on the shuttle ring gradually wears off after high‑speed rotation; the photoelectric sensor loses position signal.
Solution:
Use our special marker pen to re‑paint the worn‑out yellow mark. Allow paint to fully dry, then scrape surplus paint with a utility knife.

2. Magazine/shuttle stops running after several wire‑storage cycles
Symptom:
The shuttle halts after a few turns of wire‑loading. Some customers reported the slider failed after only 4,615 production cycles. Initially mis‑judged as sensor failure, but the machine returns to normal after slider replacement.
Possible causes:
Slider wear‑out; sensor misalignment; mechanical jamming; shuttle assembly loose.
Suggestion:
Track production count after slider replacement; keep spare sliders on‑site for quick swap. Check mechanical tightness besides sensor calibration.

3. Finished wound core cannot drop off properly
Symptom:
Wound toroidal core gets stuck and fails to fall into collection bin.
Root cause:
Material clamping claws over‑clamp the core.
Solution:
Adjust the limit screw of the clamping‑claw assembly; reduce clamping stroke so finished cores can release smoothly.
4. Slider shuts unexpectedly when moving to open position (GW‑7005 frequent complaint)
Symptom:
The slider automatically closes while moving to its open position, interrupting the wire‑loading sequence.
Solutions:
‑ Tighten loose shuttle assembly to eliminate slider slippage.
‑ Retract the relevant cylinder slightly to avoid mechanical collision against the shuttle ring.

5. Intermittent wire‑cut failure during repeated winding cycles
Symptom:
Random wire‑cut error happens in the middle of continuous winding batches. Also accompanied by wire‑hanging failure when the press‑wire unit fails to fully retract.
Solutions:
‑ Clean accumulated enamel
- Remove paint residue and burrs inside the shuttle slot with scraper tools.
‑ Make sure wool‑felt inside shuttle is firmly clamped for stable copper‑wire holding.
‑ Inspect press‑wire‑cylinder magnetic sensor for loose mounting.
6. Scrap copper wire sticks on removal unit, triggers false differential‑coil error (3×3 shuttle GW‑7004)
Symptom:
Tiny waste copper fragments stick to the scrap‑removal mechanism. When the unit moves upward, the sensor detects leftover wire and throws a differential‑coil fault alarm.
Solutions:
‑ Manually clear residual copper scraps regularly.
‑ On the HMI parameter page, locate Extend the thread removal cylinder after the remaining X turns, and change the value setting to 3.

7. Through‑beam sensor not working
Symptom: Feeding or position‑detection failure caused by a damaged through‑beam sensor transmitter head.
⚠️Warning: Cut power supply and release air pressure before wiring work.
Step‑by‑step fix:
- Open the cable protective tube and locate the through‑beam sensor cable; cut the faulty transmitter line.
- Prepare the new sensor unit, and cut off its transmitter end.
- Match and reconnect blue wire with blue wire, brown wire with brown wire. Wrap joints securely with electrical insulating tape.
- Mount the repaired new transmitter onto the machine bracket, and adjust the mounting angle until the indicator red light lights up correctly.
- Other frequent site‑reported faults (Quick reference)
- False alarm during material clamping: Clean & realign feeding‑belt through‑beam sensor, wipe dust/oil from lens.
- Machine hard to start multiple attempts: Confirm E‑stop reset, safety doors closed, air pressure at 0.5‑0.7 MPa, follow correct power‑on reset sequence.
- "Edge Delimiter Not Found" alarm: Adjust edge‑sensor sensitivity; keep shuttle yellow marker clean and intact.
- Wire fails to hook into yellow slider: Tune guide‑pin position so copper‑wire drops accurately into slider groove; check wire‑tension setting.
- Cylinders cannot fully extend/retract: Inspect magnetic‑sensor looseness, re‑position sensor trigger point and tighten screws.
- Press‑wire mechanism does not move: Verify air pressure, solenoid‑valve signal, remove mechanical blocking objects.
Note: This section offers on‑site reference guidance. A complete illustrated PDF manual will be delivered along with machine shipment. For complex electrical or mechanical breakdowns, contact our technical support team.

Package & After‑sales Support
- Export‑grade plywood wooden case for sea‑freight shipment.
- Deliverables: Illustrated operation & troubleshooting manual, spare‑parts list, electrical schematic diagram, USB program‑copy tutorial video.
- Service: Online remote technical guidance; overseas on‑site debugging upon request.
- Spare‑parts supply: Long‑term supply of consumable components: sliders, shuttle marker pens, wool felt, all types of sensors, cylinder fittings.
Request Quotation
Please share your toroidal core dimensions, copper‑wire diameter, required output per hour, and special winding requirements. We will send a formal quotation including configuration, lead‑time, and commercial terms.
You Might Also Like


